

Buyers verify eyeshadow palette pan fixation with three objective checks: a pull-out force test on sampled pans, a dimensional check of the pan against its cavity, and a visual and wipe inspection for powder residue. Typical acceptance targets are 15–30 N of pull-out resistance, a pan diameter held within ±0.05–0.10 mm, and no visible powder carry-over on the shell, rim, or cavity floor.
Those three numbers answer the question, but they only work when they are written into the purchase specification before sampling starts. Pan fixation is one of the few attributes that a filled palette can pass on the filling line and fail in the consumer's hand three weeks later, because a hot-melt bond that is adequate at 23 °C can creep at 45 °C inside a warehouse container, and a pan that sits 0.2 mm proud of the shell can look acceptable in a factory photo and feel loose in a retail tester. This guide is written for beauty brands, private-label buyers, promotional importers, and packaging procurement teams sourcing empty or filled eyeshadow palettes, blush palettes, and powder compacts from Asian contract manufacturers. It explains what pan fixation physically consists of, how each retention system behaves, which tolerances and forces to specify, how thermal aging and drop testing expose weak bonds, how to recognise the common failure modes by their symptoms, how powder cleanliness is judged, and what a defensible incoming inspection protocol looks like against ISO 2859-1.
Pan fixation is the joint that holds a pressed powder pan — the shallow metal or plastic godet that carries the eyeshadow — inside the cavity of a palette, compact, or blush case. In sourcing terms the word covers three interfaces that fail independently: the adhesive or retention bond between the pan and the cavity, the dimensional fit between the pan wall and the cavity wall, and the cleanliness of the powder and the shell after pressing and assembly. A palette is only as good as its weakest interface, and the three are usually controlled by three different departments — moulding, filling, and final assembly — which is why the failures look unrelated when they reach the buyer.
In simple terms, a palette passes pan-fixation verification when a randomly selected pan resists a defined pull-out force, sits inside a defined height band relative to the shell surface, and leaves no loose powder where a consumer will touch the product. Each of those conditions has a test method, a sampling plan, and a number attached to it. When a purchase order contains only the phrase "pans must be firmly fixed", the factory is free to interpret "firmly" as whatever its current glue setting produces, and the buyer has no basis for a claim.
The scope also depends on what is being bought. An empty palette ships as a moulded shell, a mirror, a closure, and empty cavities; the buyer or a third-party filler inserts the pans later, so pan fixation becomes a question of whether the cavity geometry and the supplied adhesive system are compatible with the buyer's own filling line. A filled palette ships with pans already bonded, which moves the entire fixation risk onto the manufacturer and makes pull-out data a legitimate incoming inspection item rather than a process note.
Four retention systems dominate volume production: hot-melt adhesive, pressure-sensitive adhesive dots, magnetic pan systems, and mechanical snap rings or friction fit. Each has a different failure signature, a different rework cost, and a different position on the cost-versus-durability curve. The choice is usually driven by palette format, target retail price, refill strategy, and the temperature profile the product will meet in distribution.
Hot-melt is the default for high-volume filled palettes. An EVA or polyolefin adhesive is melted in a heated pot or cartridge, dispensed as a ring or a bead into the cavity, and the pan is pressed in while the adhesive is still open. Pot temperature typically runs 160–180 °C, and the open time — the window between dispensing and the loss of tack — is usually 3–10 seconds, which sets the maximum cycle time of the filling line. Bead weight is normally 0.02–0.05 g per pan; below that the bond becomes spotty, above it the adhesive squeezes out aRound the pan wall and produces the visible glue ring that buyers reject on sight.
Hot-melt gives the highest consistent bond strength of the four systems, generally 15–30 N pull-out on a 26 mm pan when the dispense pattern and pot temperature are controlled. Its weakness is heat. A standard EVA softens measurably above roughly 50–60 °C, and a container that sits on a tarmac apron in summer can reach that. Polyolefin grades with higher softening points cost more and need higher pot temperatures, which in turn shortens open time and increases stringing.
Pressure-sensitive adhesive dots are pre-cut discs applied to the cavity floor and activated by the pressure of pan insertion. They remove the heated pot from the line entirely, which simplifies cleaning and eliminates burn risk and adhesive degradation from prolonged heating. Bond strength is lower, typically 8–20 N, and depends heavily on surface energy: an untreated polypropylene cavity and an anodised aluminium pan will not behave the same way, and a contaminated cavity floor — mould release agent, dust, powder — will cut the bond by half without any visible sign. PSA dots also creep under sustained load at elevated temperature, so they suit low-fill-weight pans and shorter shelf-life programmes better than large blush pans.
Magnetic systems place a magnet in the cavity floor or use a magnetic steel pan that is held by a magnet embedded in the palette body. They are the standard for refillable formats and for pro-style palettes where the consumer swaps shades. Retention force is measured as a vertical pull and typically falls in the 3–8 N range, which is deliberately lower than an adhesive bond because the pan must be removable by hand. The engineering risk moves from adhesion to rattle: a magnet that is 0.2 mm below the cavity floor, or a pan with an uneven base, will hold the pan laterally but let it buzz when the case is shaken. Magnet grade, plating, and the flatness of the pan base all need to be specified.
Mechanical retention uses an interference fit, a snap ring, or an ultrasonically welded ring that traps the pan flange. Interference is typically 0.10–0.15 mm on diameter for a plastic cavity, and the pan is pressed in with a controlled force rather than glued. There is no open time, no pot temperature, and no adhesive to age, which makes the system attractive for very long shelf life and for hot-climate markets. The trade-off is dimensional discipline: every cavity in the tool must hold its diameter, because a single low-cavity dimension turns into a loose pan on every unit from that cavity, and the defect repeats in a straight line through the shipment.
| Retention system | Typical pull-out or retention force | Process window | Behaviour after 72 h at 45 °C | Rework | Typical use |
|---|---|---|---|---|---|
| Hot-melt EVA | 15–30 N | Pot 160–180 °C, open time 3–10 s, bead 0.02–0.05 g | SMALL loss, risk of creep if grade is low | Difficult, adhesive residue | High-volume filled palettes |
| Hot-melt polyolefin | 18–30 N | Higher pot temperature, shorter open time | Best retention of the adhesive options | Difficult | Hot-climate and long-shelf-life programmes |
| Pressure-sensitive dot | 8–20 N | No heat, pressure dwell 1–3 s | Noticeable creep under load | Moderate, dot can be replaced | Small pans, short runs, low fill weight |
| Magnetic | 3–8 N vertical pull | No heat, no cure | Stable, but rattle risk if gap is uneven | Easy, by design | Refillable and pro-style palettes |
| Snap ring or interference fit | Equivalent to 12–25 N push-out | Interference 0.10–0.15 mm | Stable if moulded dimensions hold | Difficult without damage | Long shelf life, hot markets |
Whichever system is chosen, the buyer should ask for the adhesive grade data sheet, the dispense pattern drawing, and the pot temperature and open time actually used on the line — not the values in the machine manual. These three documents explain most of the variation between two suppliers quoting the same palette at the same price.

Pan fit is a dimensional problem with a narrow acceptable band. If the pan is too small, adhesive has to bridge a gap and the bond becomes a flexible column that fails in shear; if the pan is too large, it will not seat, the flange lifts, and the powder cracks when the pan is pressed. The window between those two outcomes is often less than 0.3 mm on diameter, which is why the tolerance has to be written as a number rather than described as "snug".
For standard round pans of 26 mm, 36 mm, and 57 mm, the pan outside diameter is normally specified to ±0.05 mm and the cavity inside diameter to +0.10/+0.05 mm, giving a nominal clearance of 0.05–0.15 mm per side. Buyers who accept ±0.10 mm on both sides are effectively accepting a possible 0.2 mm total variation, which is enough to change the bond from a ring to a partial arc. Ovality should be capped separately, typically at 0.08 mm, because a pan can be within diameter tolerance on two axes and still be visibly out of round, which shows as a bright crescent of glue on one side of the seam.
Cavity depth and pan height together define how far the pan rim sits below or above the shell surface. The usual target is a rim flush to 0.5 mm below the surface for a pressed powder that the consumer will touch with a brush, and up to 1.0 mm below for a palette with a protective film or a domed lid. A rim standing proud of the surface is the most common cosmetic complaint after a loose pan, because it catches on the brush and on the lid gasket, and it is the first thing a consumer notices when the palette is opened in a shop.
Aluminium pans at 0.25–0.35 mm wall thickness are the mainstream choice; tinplate is used where a magnetic base is needed, and moulded PP or PCR-PP pans appear in low-cost and refill formats. Coating matters for adhesion: anodised aluminium bonds well to hot-melt, while a heavily lacquered or oiled pan surface can act as a release layer. Where a supplier changes pan source mid-programme without telling the buyer, the first symptom is usually a drop in pull-out force on the next shipment, not a visible defect.
Bond strength is measured as pull-out force: the peak force needed to separate a cured pan from its cavity when pulled perpendicular to the cavity floor. The test is simple enough to run in a factory laboratory, but the result is only comparable between shipments if the fixture, the pull speed, the conditioning, and the sample size are fixed in the specification. A pull-out figure quoted without those four parameters is marketing, not data.
A practical method uses a stud or clamp bonded or mechanically engaged to the pan face, a tensile frame running at 10–30 mm/min, and a load cell sized so that the expected 15–30 N sits in the middle of its range. Samples are conditioned at 23 °C and 50 % relative humidity for at least 24 hours before testing, and typical sample size is five pans per colour per batch. The report should give the mean, the minimum, and the failure location — adhesive failure at the pan interface, adhesive failure at the cavity interface, or cohesive failure inside the glue line. Cohesive failure at a lower force is often a better sign than adhesive failure at a higher one, because it means the bond to both surfaces is stronger than the adhesive itself.
The acceptance band most buyers settle on is 15 N minimum with a 20–25 N target mean for a standard 26 mm pan, and 25–30 N for larger blush pans carrying more powder mass. A single result below the minimum should trigger a retest of ten pans from the same batch, not an immediate rejection, because fixture alignment and pan surface contamination can produce one-off lows. Two consecutive lows, or a mean that has drifted more than 20 % from the approved golden sample, is a process signal and should hold the shipment.

Room-temperature pull-out data tells a buyer what the palette can do on the day it is packed. It says very little about what happens after four weeks in a container, a truck, and a retail back room. Thermal aging and drop testing are the two laboratory proxies that correlate best with field failures, and both are cheap enough that there is no good reason to skip them on a first order.
The standard thermal aging cycle for a pressed powder palette is 45 °C for 72 hours, either in a dry oven or in a stability chamber at ambient humidity. After the cycle the samples return to 23 °C for two hours and are re-tested for pull-out force. An acceptance criterion of no more than 20–25 % loss against the pre-aging mean is realistic for hot-melt systems; a pressure-sensitive dot will often lose more, and a magnetic system should lose almost nothing. The same samples should be inspected for glue squeeze-out, pan lift, powder oil migration, and any change in the mirror coating or the case closure.
Drop testing is usually a 1.2 m free fall onto a rigid floor, one drop per corner, per long edge, per short edge, and per face, for ten drops per sample, with the palette closed as it would ship. After each drop the case is opened and checked for pan displacement greater than 0.3 mm, audible rattle, powder cracking, and lid or clasp damage. A palette that survives pull-out but shifts a pan on the third corner drop has a fit problem, not an adhesive problem, and the fix belongs in the mould rather than in the glue pot.
Most pan fixation complaints fall into six patterns, and each has a signature that can be recognised without a laboratory if the inspector knows what to look for. Reading the failure backwards — from symptom to root cause — is the fastest way to decide whether a shipment needs rework, a process correction, or a tooling change.
| Failure mode | What the buyer sees | Likely root cause | Detection at incoming inspection |
|---|---|---|---|
| Loose pan in service | Pan rattles or lifts after transit; powder cracks radially | Bead weight below 0.02 g, cold cavity, short open time, contaminated pan base | Pull-out test at 15 N minimum; shake test at 2 Hz for 30 s |
| Glue squeeze-out | Visible adhesive ring on the pan wall or cavity rim | Bead weight above 0.05 g, excessive insertion force, cavity depth shallow | Visual at 500–1000 lux with a 3× loupe; wipe test on the rim |
| Stringing | Fine adhesive threads bridging pan and shell | Pot temperature too high, nozzle stand-off too long, retraction setting wrong | Visual on first-off and every hour; count threads per 100 pans |
| Pan proud of surface | Rim catches brush; lid does not close flush | Cavity depth out of tolerance, pan height over spec, adhesive layer too thick | Height gauge at four rim points; go/no-go flush gauge |
| Powder carry-over | Loose powder on shell, mirror, or cavity floor | Static, poor air blow-off, overfill, brushing after pressing | white-glove wipe and tape lift on 5 % of the sample |
| Pan rotation | Round pan spins freely in a round cavity | Clearance too large with no anti-rotation feature; adhesive only on the base | Torque test by hand; mark and rotate through 90° on ten pans |
Two of these deserve emphasis because they are frequently misdiagnosed. Pan rotation is not a bond failure — the pan is still attached — but it misaligns embossed logos and, in a split-pan layout, can rotate a shade out of its labelled position. The fix is either an anti-rotation tab in the cavity or a bead pattern that contacts the pan wall rather than only the base. Powder carry-over, meanwhile, is usually blamed on the filler when it originates upstream in the press: an overfilled pan that is struck off with a blade leaves a ridge that crumbles during insertion, and no amount of downstream air blowing will remove powder that is still being generated.
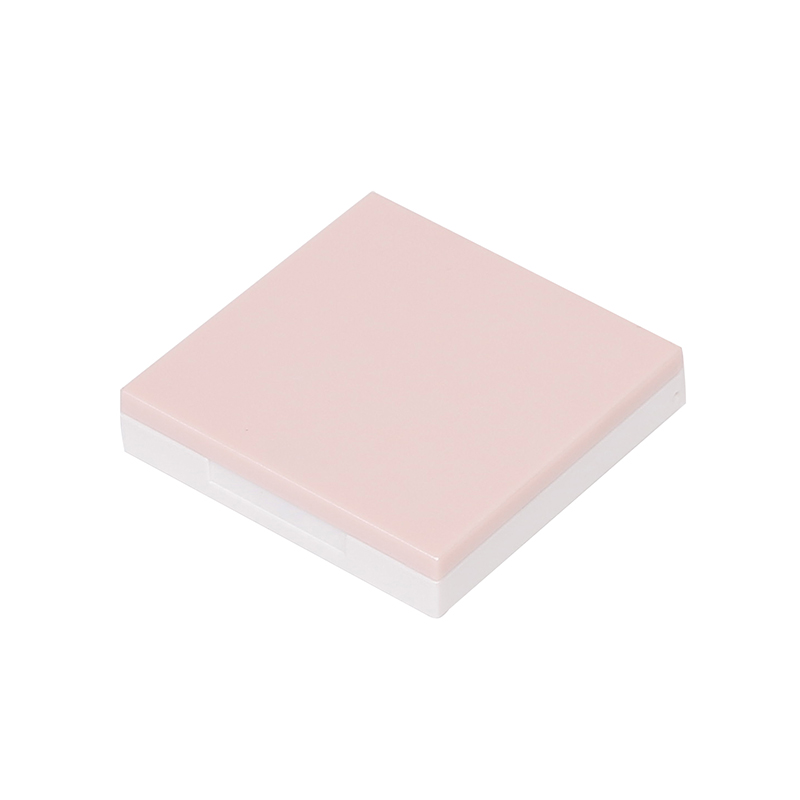
Powder cleanliness is judged on three surfaces: the pan rim and the shoulder immediately around it, the cavity floor and the gaps between cavities, and the mirror and inner lid. The acceptance definition should be written as "no visible powder residue on any surface the consumer touches, viewed at 500–1000 lux from 30 cm, with and without a 3× magnification", because "clean" without a lighting condition and a viewing distance is not a test.
The primary check is visual under defined lighting, performed on the finished unit with the lid open. A white glove or a lint-free white cloth is then wiped across the shell shoulder and the inner lid; any colour transfer on the cloth is a defect, and the cloth becomes the photographic evidence for the claim. A tape lift on the mirror and the cavity floor catches fine particles that the eye misses, and it is the only reliable way to detect transfer from a very light shade onto a black shell.
Most residual powder is held by static rather than by gravity, particularly on PP and ABS shells in dry production rooms. Effective lines use ionised air, a controlled blow-off pressure, and an extraction hood at the filling station; ineffective lines use a plain air gun that moves the powder from the cavity to the mirror and calls it cleaning. Humidity below about 35 % relative humidity makes static worse, so a dry winter week can produce a spike in carry-over defects with no change in the process.
In multi-shade palettes, cross-contamination between adjacent cavities is a separate defect class. A dark shade that bleeds into a light neighbour during pressing, or a brush that is used across cavities without cleaning, produces a palette that looks unclean on opening even when each pan is individually correct. Buyers should ask for the line's colour-change procedure and the number of palettes scrapped at each changeover, because that number is the most honest indicator of how seriously cleanliness is managed.
An inspection protocol converts the specification into a decision rule: how many units to pull, which attributes to check, and how many defects are allowed before the lot is rejected. Attribute sampling to ISO 2859-1, single sampling, normal inspection, general inspection level II, with AQL 2.5 for major defects and AQL 4.0 for minor defects, is the most widely understood framework and the easiest to defend in a supplier conversation.
Major defects in this product category are the ones that stop the palette being sold: a pan that fails pull-out, a loose or rotating pan, a pan proud of the surface, visible glue on the rim, powder carry-over on the mirror, and any closure or hinge failure. Minor defects are cosmetic: slight shade variation, a light glue smear inside a cavity that is covered by the pan, minor scuffs on a matte shell. The distinction matters because a shipment rejected on minor defects alone is usually negotiable, while one rejected on major defects is not.
| Lot size (pcs) | Code letter | Sample size | AQL 2.5 major (Ac/Re) | AQL 4.0 minor (Ac/Re) |
|---|---|---|---|---|
| 501–1,200 | J | 80 | 5 / 6 | 7 / 8 |
| 1,201–3,200 | K | 125 | 7 / 8 | 10 / 11 |
| 3,201–10,000 | L | 200 | 10 / 11 | 14 / 15 |
| 10,001–35,000 | M | 315 | 14 / 15 | 21 / 22 |
Pull-out testing is destructive and cannot be applied to a 200-piece sample. The practical compromise is to run it as a separate, smaller test — five pans per colour per batch, drawn from the same lot — and to treat any individual result below 15 N as a major nonconformity that escalates the whole lot to a 100 % functional check or a hold. Visual and dimensional checks follow the sampling table; the destructive tests follow the batch.

Pan fixation specifications are only enforceable if the order structure supports them. A buyer who orders 3,000 pieces across twelve shades is asking the factory to run twelve adhesive and insertion set-ups, and each set-up is a chance for the pot temperature or the bead weight to drift. Typical minimum order quantities for custom palettes sit at 3,000–5,000 pieces, with 500–1,000 pieces per colour; below 500 pieces per shade, most factories will either refuse the shade or absorb it into a larger run and hand-fill it, which is exactly where pan fixation defects cluster.
Batch coding should identify the moulding date, the filling date, the adhesive lot, and the shade. The adhesive lot matters more than buyers expect: two lots of the same grade can differ in open time enough to shift pull-out force by several newtons, and without the lot number on the carton a failure cannot be traced back to a delivery. Coding is normally inkjet on the carton and laser or pad-printed on the palette base, and both should be legible after the drop test — a code that rubs off in transit is not a traceability system.
Export cartons for filled palettes are usually 5-ply K=K corrugated, with an inner tray or partition that stops palettes touching each other, and a polybag only where the shell finish is sensitive to scuffing. Carton drop testing at 1.2 m on the bottom edge and one vertical edge, followed by an internal inspection, is the minimum evidence that the pack survives handling. Buyers should also specify pallet pattern, maximum carton weight — commonly 12–15 kg for manual handling — and whether the carton carries a shipping mark with the batch code repeated on two adjacent panels.
A specification that survives a change of shift, a change of adhesive lot, and a change of project engineer is short, numeric, and testable. The following list is the minimum content for a pan fixation clause that a factory can actually work to and a third party can actually verify.
For a standard 26 mm pan, 15 N is a reasonable minimum and 20–25 N is a practical target mean, measured perpendicular to the cavity floor at a pull speed of 10–30 mm/min after 24 hours of conditioning at 23 °C and 50 % relative humidity. Larger blush pans carrying more powder mass usually need 25–30 N. Magnetic and refillable systems are intentionally lower, typically 3–8 N, because the pan must be removable by hand. Always specify the fixture, speed, sample size, and conditioning alongside the number, otherwise results from two suppliers cannot be compared.
Most late failures are heat-related creep rather than an initially weak bond. A hot-melt adhesive that tests well at 23 °C can soften inside a container that reaches 50 °C or more, and a pressure-sensitive dot will creep under the sustained load of a heavy pan. The other common cause is contamination: mould release agent, dust, or powder on the cavity floor reduces adhesion without showing up on a visual check. Thermal aging at 45 °C for 72 hours, followed by a pull-out re-test, reproduces most of these failures before shipment.
A clearance of 0.05–0.15 mm per side works for most adhesive-bonded palettes, achieved with a pan diameter tolerance of ±0.05 mm and a cavity diameter of +0.10/+0.05 mm. Tighter than that and the pan will not seat without excessive force, which squeezes adhesive out and lifts the rim. Looser than that and the adhesive has to bridge a gap, which turns a shear joint into a flexible column that fails under drop. Interference-fit and snap-ring systems invert the logic and typically use 0.10–0.15 mm of interference instead of clearance.
Define the lighting, the viewing distance, and the surfaces first: 500–1000 lux at 30 cm, checking the pan rim, cavity floor, shell shoulder, mirror, and inner lid. Then add two physical checks — a white lint-free glove wipe across the shoulder and inner lid, and a tape lift on the mirror and cavity floor. Any colour transfer on the cloth or tape is a defect. Photograph every finding next to the batch code. Visual inspection alone tends to miss fine transfer from light shades onto dark shells, which is exactly the defect consumers notice first.
It needs different acceptance criteria, not less testing. Pull-out is replaced by vertical retention force, typically 3–8 N, and the critical defect becomes rattle rather than debonding. Test by shaking the closed palette for 30 seconds and listening, then check lateral movement by hand. Magnet grade, plating thickness, and pan base flatness all affect the result, and a 0.2 mm gap between magnet and pan is enough to hold the pan laterally while letting it buzz. Drop testing still applies, with the same 1.2 m height and 0.3 mm displacement limit.
Use ISO 2859-1, general inspection level II, single sampling, normal inspection, with AQL 2.5 for major and 4.0 for minor defects. That gives 80 units for a lot of 501–1,200 pieces, 125 for 1,201–3,200, and 200 for 3,201–10,000. Destructive pull-out testing runs separately at five pans per colour per batch, because it cannot be applied to a 200-piece sample. Record every result against the batch code so that a failure can be traced to a specific adhesive lot, filling shift, or mould cavity.
Pan fixation is a three-part problem disguised as one. The adhesive or magnet decides whether the pan stays put, the dimensional fit decides whether the bond has anything to hold onto, and the cleanliness of the powder and shell decides whether the consumer trusts the product when the lid opens. Buyers who test only one of the three usually discover the other two in the claim data six weeks after the container lands.
The verification path is straightforward and does not require an in-house laboratory: write numeric acceptance criteria into the purchase specification, run pull-out at 15 N minimum with a 20–25 N target, age samples at 45 °C for 72 hours and re-test, drop at 1.2 m and measure pan displacement against a 0.3 mm limit, and inspect powder cleanliness under defined lighting with a glove wipe and a tape lift. Sample to ISO 2859-1 at AQL 2.5 major and 4.0 minor, keep destructive tests on a separate batch basis, and hold a signed golden sample. Order in the 3,000–5,000 piece range with 500–1,000 pieces per colour so that each shade gets a proper set-up, and ship in 5-ply K=K cartons with the batch code and adhesive lot traceable on two panels. A supplier that can supply those numbers, and the records behind them, is a supplier whose palettes will still hold their pans after the first summer in transit.
Цзиньхуа Синцяо Пластиковая Промышленность Лтд.
 Мобильный телефон: +008613868982062.
 Телефон: +86-579-82196667
 Факс: +86-579-82196656
 Электронная почта:sales@zjxqpackaging.com
 Веб-сайт:http://www.zjxqpackaging.com
 Адрес: нет. 377, улица Юнсюэ, городской округ W, город Цзинь, провинция Цзэ Хэцзян
Copyright © 2022 Компания Цзиньхуа Синцяо Пластиковая Промышленность Лтд.
Этот веб-сайт использует файлы cookie, чтобы обеспечить вам максимально эффективное использование нашего веб-сайта.
 English



 телефон
Комментарий
(0)